MaintenanceSep 10, 2026
Preventive Maintenance: What It Is and How to Implement It
What preventive maintenance is, how to set frequencies without copying the manufacturer's manual, which indicators measure it and when it makes sense to move to predictive. With an Excel template.
What preventive maintenance is #
Preventive maintenance is servicing equipment at planned intervals (by elapsed time or by hours of use) before it fails, without waiting for a symptom to appear. It answers a very specific question: how long can this asset run before the probability of failure rises enough that it is worth stopping it on purpose?
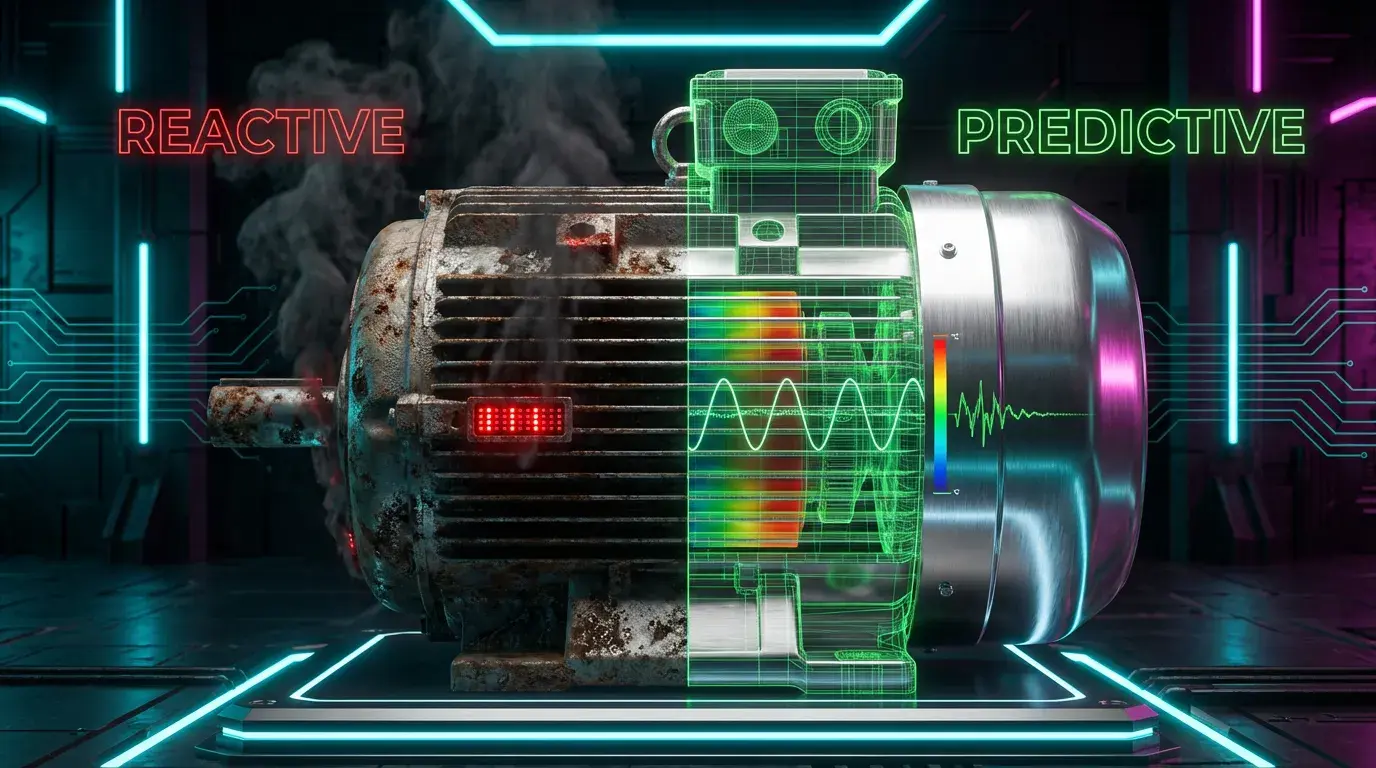
It differs from its two neighbors in when it acts. Corrective maintenance repairs after the failure. Predictive maintenance measures the equipment's actual condition and acts when that measurement indicates degradation. Preventive maintenance acts by the calendar, whether or not it knows the equipment needed it. For the full map of the four types and which one fits each asset, see the guide to types of industrial maintenance.
The mistake almost every plan carries #
In most of the plants we visit, the plan was born the same way: someone copied the frequencies from the manufacturer's manual, loaded them into a spreadsheet, and since then they have been carried out out of habit. Nobody looked at them again.
The manufacturer's manual is an honest but generic starting point: it is written for an average unit, in average conditions, with an average duty cycle. Your plant is not average. The same motor running two shifts in an environment with flour dust does not have the same interval as that motor running one shift in a clean room. Copying the manual without adjusting it produces two errors at once: over-maintaining lightly loaded equipment, spending labor hours opening things that were fine, and under-maintaining heavily loaded equipment, which keeps failing between interventions.
How to really adjust a frequency
- Start from the history, not the manual. If the equipment has been in the plant for a year, its own failures tell you more than the datasheet. How long it lasted between stops, what broke and what condition it was in.
- Correct for duty cycle and environment. Shifts, load, temperature, humidity, dust and vibration transmitted from neighboring equipment. These are the factors that shorten real life compared with theoretical life.
- Adjust based on what you find. If three interventions in a row found the component in good condition, the interval is too short. If two out of three found advanced wear, it is too long.
How to build a preventive maintenance plan #
A plan that works has five pieces, in this order.
1. Asset inventory with criticality
Not all equipment deserves the same effort. Classify by consequence of failure: what an hour of downtime on that asset costs, whether there is redundancy, whether it affects safety or regulatory obligations. Critical assets concentrate the plan; low-consequence ones can be deliberately run to failure with a spare on hand, which is planned corrective maintenance and a valid decision, not negligence.
2. Failure modes, not inherited tasks
For each critical asset, write down how it breaks: bearing by fatigue, seal by temperature, belt by misalignment. Every task in the plan must address an identified failure mode. If a task has no associated failure mode, it is ritual, not maintenance. Most plants discover at this step that a third of their preventive tasks address nothing.
3. Corrected frequencies
Using what was covered in the previous section. And with a practical rule: it is better to start with a short interval and lengthen it with evidence than to start long and find out through a production stop.
4. Resources and window
Each task needs a spare part, a tool, qualified staff and a window in which production allows the intervention. A plan that ignores the window falls apart on its own, and a plan that is systematically skipped trains the team to ignore it.
5. Record of what actually happened
This is where most plans fall down. If execution is not recorded (what was done, how long it took, what condition the component was in), the plan cannot improve, because there is nothing to adjust the frequencies in step three with. The record is what turns the plan into a loop instead of a static list.
📥 Template to build it
The preventive maintenance plan Excel template includes the fields from this article: inventory with criticality, failure mode per task, frequency, owner and execution log.
Examples of preventive maintenance in a plant #
To keep it from staying abstract, here are five real tasks with their associated failure mode:
- Motor bearing lubrication every 2,000 hours. Addresses fatigue from a degraded lubricant film, the most common failure mode in continuous-process motors.
- Belt tension and alignment check every month. Addresses premature wear from misalignment, which also transmits vibration to the rest of the drive train.
- Cleaning heat exchangers and condensers each season. Addresses loss of heat transfer due to fouling, which shows up as rising electrical consumption before it shows up as a stop.
- Thermography of electrical panels every six months. Addresses hot spots from loose connections, a frequent cause of electrical room fires.
- Checking process sensors against a calibrated reference, annually. Addresses instrument drift, which does not stop the line but corrupts every decision you make with that data.
Locked file
oee-calculation-template.xlsx
Leave your work email to download this spreadsheet and hear about the next one.
Advantages and disadvantages, without embellishment #
In favor: it reduces unplanned stops, lets you plan spare parts and staffing instead of improvising, extends asset life and brings order to the operation. In plants coming from pure corrective work, the effect on the maintenance team's morale is immediate: they stop firefighting.
Against: it services equipment that was healthy, and every opening introduces its own risk of infant-mortality failure. It consumes labor hours on tasks that were not always necessary. And it has a structural blind spot: the failure that appears between two scheduled interventions goes unseen. That blind spot is exactly what predictive maintenance with IoT covers.
How to know if your preventive plan is working #
The indicator almost every plant uses is schedule completion: what percentage of planned tasks was carried out. It is useful for knowing whether the team is doing its job, and useless for knowing whether the plan works.
What measures the result is something else:
- A drop in emergency corrective work. If preventive maintenance is working, unplanned work orders go down quarter after quarter. If they do not, the plan is addressing failure modes that are not the ones breaking your production.
- Rising MTBF and stable or falling MTTR. Mean time between failures should get longer. How they are calculated, with an example, is in the guide to industrial reliability: MTBF, MTTR and availability.
- Availability of the critical asset. It is the number production cares about and the only one that translates maintenance into business language.
A plan with 100 % completion and the same number of unplanned stops as last year is not working, however green the dashboard looks.
When preventive maintenance is no longer enough #
Preventive maintenance has a ceiling, and it is worth recognizing it before you hit it. It makes sense to move to predictive when two conditions are met at the same time: downtime on the asset costs more than instrumenting it, and the failure gives measurable signals before it happens (vibration, temperature, electrical consumption, acoustic signature).
If either one is missing, preventive maintenance is still the right answer. For cheap, redundant assets or those with sudden failures and no prior signal, instrumenting is overspending. The detailed comparison, with costs, is in predictive vs. preventive maintenance.
From the spreadsheet to the system #
Excel is enough to get started and for small plants. It stops being enough when any of these three things happens: the file lives on one person's computer and nobody else knows which version is the right one; there is no history because someone deleted last year's rows to tidy up; or the plan does not send reminders, and completion depends on someone remembering to open the file.
That is where a CMMS with condition data comes in: work orders are generated automatically against the plan, the history is kept per asset and the indicators are calculated from closed work orders and equipment signals. Deciding what to do with those indicators is still the planner's job; what changes is that they stop losing hours assembling the number and spend them deciding.
Related reading #
Topics
- preventive maintenance
- what is preventive maintenance
- preventive maintenance plan
- preventive maintenance examples
- pm frequency
- preventive maintenance kpis
- preventive vs predictive maintenance
- preventive maintenance excel template
About the author
Víctor RuzCEO
Automation and Robotics Engineer (Universidad Andrés Bello, 2012). More than twelve years in robotics and industrial automation. Founder and CEO of iGromi, where he connects machines, systems and plant people with secure industrial AI.