MaintenanceSep 7, 2026
Types of Industrial Maintenance: 2026 Guide + Excel Plan
Corrective, preventive, predictive and proactive: what each type of maintenance is, when it makes sense, how to combine them by asset criticality, and an Excel template to build the plan.
Locked file
plantilla-plan-mantenimiento-preventivo-v2-en.xlsx (210 KB)
Leave your work email to download this spreadsheet and hear about the next one.
Why it matters to tell the types of maintenance apart #
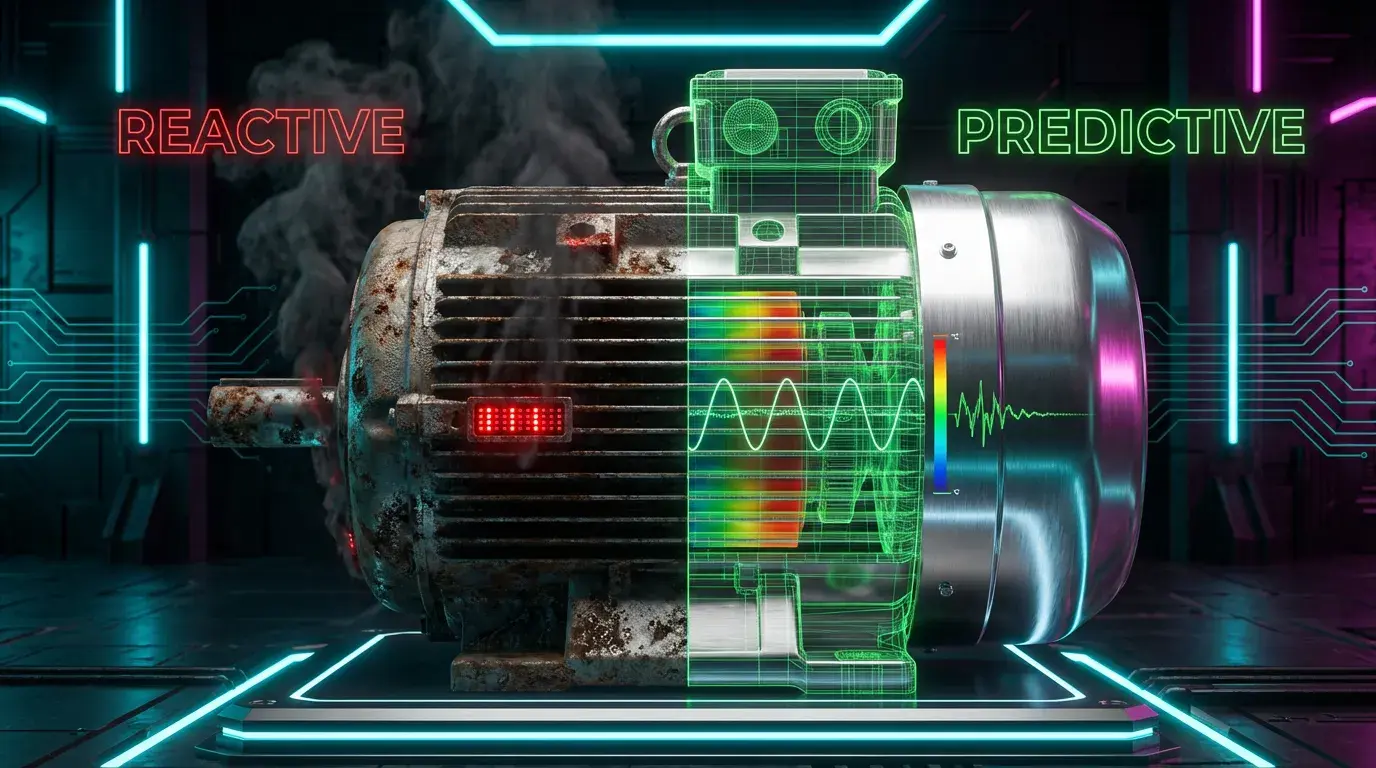
In almost every plant we visit, the maintenance plan was born the same way: someone copied the frequencies from the manufacturer's manual, loaded them into a spreadsheet, and since then they have been carried out out of habit. The result is well known: equipment that was fine gets serviced, equipment about to fail slips through, and the maintenance team lives firefighting. Choosing the right type of maintenance for each asset is the decision that weighs most on total cost and on line availability. Preventive maintenance, the most widely used of the four, is covered separately in what preventive maintenance is and how to implement it.
This guide explains the four basic types, the two frameworks used to combine them and a practical criterion for assigning them. If you only want the tool, the maintenance plan Excel template already comes with the fields to classify each task.
The four types of maintenance, in one table #
| Type | When it intervenes | What it needs | Where it makes sense |
|---|---|---|---|
| Corrective | After the failure | Spare parts and staff available | Cheap or redundant assets, or failures with no consequence |
| Preventive | At intervals of time or usage | Defined frequencies and execution discipline | Predictable wear: lubrication, filters, belts |
| Predictive | When the measured condition calls for it | Sensors, thresholds and someone to interpret the trend | Critical equipment whose failure gives measurable signals |
| Proactive | Before the failure mode exists | Root cause analysis and redesign | Repetitive failures with an identifiable cause |
1. Corrective maintenance #
It means repairing or replacing after the equipment has failed. It has a bad reputation, but there is a legitimate version: planned corrective maintenance, where you decide in advance to let a component fail because preventing the failure costs more than replacing it, and you have the spare part and procedure ready. What destroys the operation is emergency corrective maintenance: the unforeseen failure that stops the line, forces rush purchases of spare parts and consumes the team's hours at the worst possible moment.
The metric that reveals the problem is the percentage of labor hours spent on unplanned corrective work. Above 30 percent, the preventive plan is not working or does not exist.
2. Preventive maintenance #
It intervenes at fixed intervals, either by time (every month, every quarter) or by usage (every 500 hours, every 10,000 cycles). It works very well where wear is predictable: lubrication, filter changes, belt tensioning, calibrations. Its limit is that it does not know whether the equipment needs it: a bearing with months of useful life left gets replaced, or you arrive too late to one that degraded faster than normal because of an overload.
Two frequent mistakes: copying the manufacturer's frequencies without adjusting them to the plant's real duty cycle, and measuring preventive maintenance by tasks closed instead of failures avoided. A preventive plan is judged by the drop in emergency corrective work, not by how closely the calendar was followed. In the comparison of preventive and predictive maintenance we explain when preventive is no longer enough.
3. Predictive maintenance #
It intervenes when the equipment's measured condition justifies it. The signals most used on plant floors are vibration in motors and bearings, temperature in bearings and electrical panels, electrical current in motors and pumps and, more recently, acoustic signature. Each one anticipates a different failure mode: vibration detects imbalance, misalignment and bearing damage weeks before breakage; current reveals overloads and mechanical wear; temperature shows friction and electrical problems.
Predictive maintenance requires three things that are often underestimated: a sensor installed at the right point, a baseline of the healthy equipment to compare against and a person who decides what to do with the trend. The technology counts the micro-stops and proposes the intervention; the maintenance team creates and executes the work order. To go deeper, see the guide to predictive maintenance with IoT and vibration analysis. If you are choosing software to manage it, compare the Fracttal alternatives and Tractian.
4. Proactive maintenance #
It does not try to detect or anticipate the failure but to eliminate its cause. If a bearing fails every four months, predictive maintenance will replace it just in time every four months; proactive maintenance asks why it lasts four months and discovers the coupling misalignment, the contaminated lubricant or the line overload. Its tools are root cause analysis, FMEA and redesign. It is the most profitable type and the least practiced, because it requires engineering time that emergency corrective work eats up first.
TPM and RCM: how to decide the mix #
The four types do not compete; they combine. Two frameworks help decide the proportion:
- RCM (reliability-centered maintenance) starts from the asset's functions and the consequences of each failure mode to assign the task that actually reduces risk. It is the method for deciding which asset goes to predictive, which to preventive and which is run to failure.
- TPM (total productive maintenance) divides responsibilities: the operator handles basic care and daily inspection, maintenance focuses on planned and predictive work, and both measure the result with OEE.
A practical criterion: criticality vs. cost of intervention #
Place each asset on a two-axis matrix. On the first axis, the consequence of failure: safety, quality, line stop or nothing relevant. On the second, whether the failure gives measurable signals before it happens. With that, the assignment almost falls out on its own:
- High consequence and a failure with a measurable signal: predictive.
- High consequence and a failure with no signal (electronics, sudden fatigue): time-based preventive plus redundancy.
- Low consequence: planned corrective with a spare in the storeroom.
- Repetitive failure in any category: proactive before anything else.
How to measure whether the mix works #
Four indicators are enough to start: MTBF (mean time between failures), MTTR (mean time to repair), availability and work order backlog. We explain them with formulas and a worked example in the guide to industrial reliability. If MTBF goes up and emergency corrective work goes down, the mix is right even if the preventive calendar is followed less closely.
Start with the template #
The maintenance plan Excel template includes a maintenance-type column per task, asset criticality and frequency. Use it to classify what you currently do out of habit; most plants discover that a third of their preventive tasks have no associated failure mode. When the spreadsheet falls short, the next step is a CMMS with condition data, not another spreadsheet.
Frequently asked questions #
What are the types of industrial maintenance?
The four basic types are corrective (repair after the failure), preventive (service by time or usage), predictive (service based on the equipment's measured condition) and proactive (eliminate the root cause of the failure). TPM and RCM are not types but methodologies for deciding how to combine them.
What is the difference between preventive and predictive maintenance?
Preventive maintenance acts at fixed intervals of time or usage, without knowing whether the equipment needs it. Predictive maintenance measures actual condition (vibration, temperature, current, acoustics) and schedules the intervention only when a signal indicates degradation.
Which type of maintenance is best?
None on its own. The right combination depends on the asset's criticality and the cost of its failure: planned corrective for cheap, redundant equipment, preventive where failure is predictable from wear, predictive where downtime is expensive and the failure gives measurable signals.
What is planned corrective maintenance?
It is deliberately letting equipment fail because repairing it afterward costs less than preventing the failure, but with spare parts, procedure and staff already defined. It differs from emergency corrective maintenance, which is the unforeseen failure that stops production.
Topics
- types of maintenance
- types of industrial maintenance
- corrective maintenance
- preventive maintenance
- predictive maintenance
- proactive maintenance
- planned corrective maintenance
- maintenance strategy
About the author
Víctor RuzCEO
Automation and Robotics Engineer (Universidad Andrés Bello, 2012). More than twelve years in robotics and industrial automation. Founder and CEO of iGromi, where he connects machines, systems and plant people with secure industrial AI.