Plant StrategyApr 22, 2026
CMMS Software for Manufacturing: How to Choose Beyond Excel
Excel and 1990s CMMS share one flaw: they depend on people typing data after the failure. How to evaluate a CMMS for manufacturing with edge AI.

Locked file
matriz-evaluacion-cmms-en.xlsx (12 KB)
Leave your email to download this free spreadsheet and hear about the next one.
The CMMS as a Financial Liability #
Most factories in Latin America manage maintenance with one of two methods: spreadsheets (Excel) or a 1990s-era CMMS for manufacturing (Computerized Maintenance Management System), such as SAP PM or other legacy software.
Both methods share the same architectural flaw: they depend entirely on people entering the data.
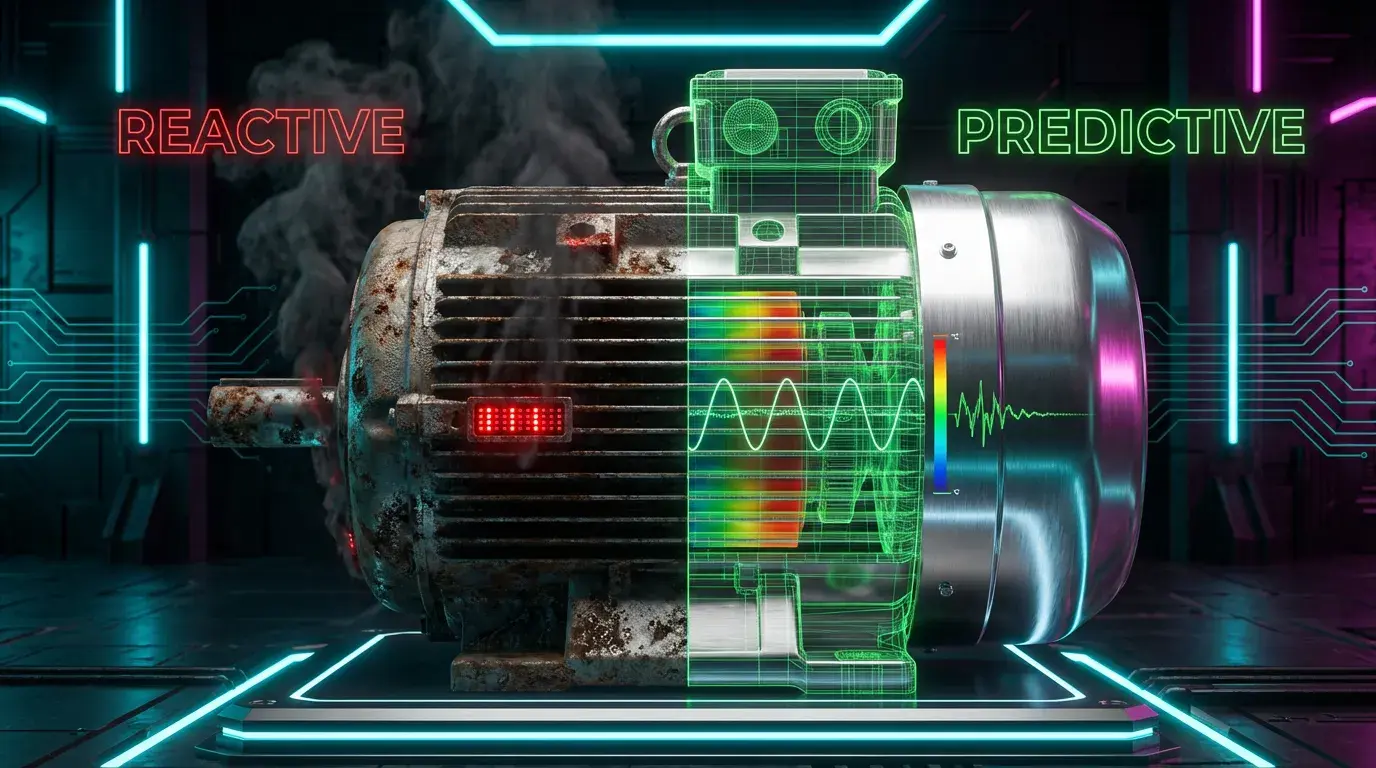
A traditional CMMS works like a historical database. It tells you which machine failed, which spare part was used and how long the technician took to fix it. But all of that information arrives after the damage is done. In Industry 4.0, if your system can't stop the failure before it happens, it's a liability.
From Reactive to Predictive #
The real technology leap for modern manufacturing isn't buying a prettier CMMS; it's implementing an Edge AI architecture (intelligence at the source).
Instead of a technician noting on a tablet that the motor is vibrating too much, the IoT sensor on the motor talks directly to the Edge Computing node. The AI analyzes the spectral pattern of the vibration, estimates, for example, that the bearing will fail within 14 days, and drafts the work order in the CMMS along with the spare-part request to the ERP, for a planner to approve.
The Per-License Cost Trap
Traditional CMMS platforms charge per user seat or per module. That discourages collaboration: if you want all 50 line operators to be able to report failures, the license bill quickly gets out of hand.
When you evaluate a CMMS, ask how the cost grows as you add users and sensors. With iGromi, operators reporting failures are not charged as extra seats; ask us how the model fits your plant.
How Do You Choose CMMS Software for a Manufacturing Plant? #
In five steps, in this order. The order matters more than the feature list:
- Set the weights before looking at candidates. If you adjust them afterwards, you will be fitting them to the one you already liked.
- Score from 0 to 5 based on what you saw in a demo on your own equipment, not on what the proposal says. 0 means it does not do it, 3 that it does it with limitations and 5 that it does it well.
- Ask everyone the same questions, in the same meeting, and write down the answer word for word. An evasive answer is data too.
- Work out the three-year cost: license, commissioning, hardware, integrations, migration, training, support and your own team's hours. The proposal shows year one; the decision is made on all three.
- Compare score and cost per asset together. The cheapest option with a low score is abandoned by month six and paid for twice.
Which Criteria Matter When Evaluating a CMMS for Manufacturing? #
| Criterion | Why it matters in a plant |
|---|---|
| Where the data comes from | Whether the technician types it in or it arrives from the machine. It decides whether the system is still alive in month six. |
| Work orders | Create, assign, close and keep evidence, with photo and signature if the process requires it. |
| Preventive plans | By calendar, by run hours and by equipment condition. All three, not just the first. |
| Integration with what is installed | PLCs, sensors, ERP and API: what it reads natively and what needs development. |
| License model | Per user, per asset, per tag or flat. It decides whether adding operators and sensors has to go through purchasing. |
| Inventory and spare parts | Stock, reorder point and cost per asset. |
| Mobility on the floor | The technician closes the order next to the machine, not back at the office. |
| Reports and KPIs | MTBF, MTTR, plan compliance and cost per asset, without exporting to Excel to calculate them. |
| Offline operation | What happens during a full shift with the link down. |
| Local support | In your language and time zone, with someone who can come on site. |
| Migrating what you already have | The history in Excel or the previous system: how much is recovered and how fast. |
The weights depend on the plant. A food plant with frequent audits will weight evidence on work orders more heavily; a remote site, offline operation. This article's free matrix includes the eleven criteria with editable weights and calculates each candidate's weighted total.
What Should You Ask a CMMS Vendor? #
Ten questions that separate candidates better than any brochure:
- What happens if the internet goes down for a whole shift?
- Does the price change if I connect 50 more sensors next year?
- Can I take all my data with me if I leave? In what format and how fast?
- How many plants in my country use it today, and can I talk to one?
- Who does the commissioning: you or a third-party integrator?
- Does the technician need a signal inside the building to close an order?
- Which protocols does it read natively and which need development?
- What happens to the history I already have in Excel?
- How many weeks after signing until I close the first real work order?
- Which part of the price is paid once and which part repeats every year?
How Do You Evaluate a CMMS for a Company with Several Plants? #
With the same matrix, on two levels. Weights are agreed once at headquarters, so every plant evaluates with the same yardstick. Scoring is done at each plant, with its own equipment and its own link, because the candidate that works well at the plant with good fiber may fail at the one in a valley with no signal. Three points weigh more than at a single site: a common asset coding scheme, each plant being able to operate without depending on the corporate network, and KPIs that can be compared across sites without rebuilding them in Excel.
When Should You Move from Excel to a CMMS? #
When the spreadsheet stops answering in time: the preventive plan falls behind without anyone noticing, orders are closed from memory at the end of the shift, or calculating one machine's MTBF takes an afternoon. If you are still on the spreadsheet, the industrial maintenance guide explains the types, how to build the plan and which KPIs to track before making the jump. To see how iGromi handles it, there is the CMMS software page.
Frequently Asked Questions #
What is a CMMS for manufacturing?
It is a computerized maintenance management system built for plants: it records assets, work orders, preventive plans, spare parts and KPIs such as MTBF and MTTR.
Which CMMS software suits a mid-sized manufacturer?
The one that scores best on your matrix with your plant's weights, not the best-known one. At a mid-sized company, the license model, mobility on the floor and migrating the Excel history usually weigh more than advanced modules.
How long does a CMMS implementation take?
Ask for it as a commitment: how many weeks after signing until the first real work order is closed. Projects drag on during commissioning, not during the sale.
Topics
- cmms for manufacturing
- cmms software
- cmms evaluation
- maintenance management software
- cmms vs excel
- predictive maintenance cmms
About the author
Víctor RuzCEO
Automation and Robotics Engineer (Universidad Andrés Bello, 2012). More than twelve years in robotics and industrial automation. Founder and CEO of iGromi, where he connects machines, systems and plant people with secure industrial AI.